Inquire: Call 0086-755-23203480, or reach out via the form below/your sales contact to discuss our design, manufacturing, and assembly capabilities.
Quote: Email your PCB files to [email protected] (Preferred for large files) or submit online. We will contact you promptly. Please ensure your email is correct.
Notes: For PCB fabrication, we require PCB design file in Gerber RS-274X format (most preferred), *.PCB/DDB (Protel, inform your program version) format or *.BRD (Eagle) format. For PCB assembly, we require PCB design file in above mentioned format, drilling file and BOM. Click to download BOM template To avoid file missing, please include all files into one folder and compress it into .zip or .rar format.
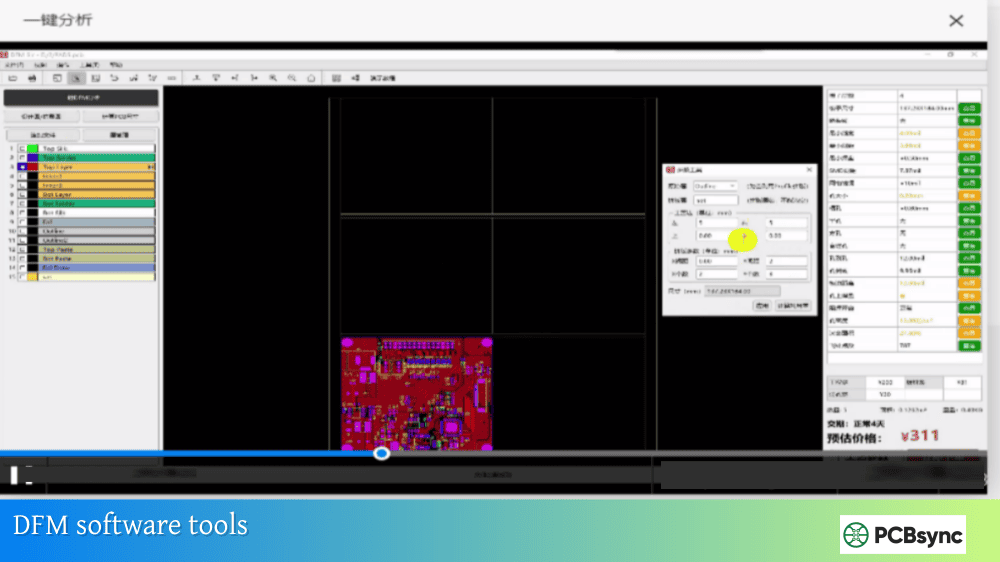
Use these 25 PCB DFM checks to review drills, copper, planes, mask and legend before release. Record each finding against the actual board revision and the supplier-reviewed construction, rather than adopting generic minimum dimensions.
This short worksheet complements the detailed checklist below. Use supplier-approved limits for your material, copper, hole structures and acceptance requirements. A calculator or generic table cannot approve the complete construction.
6 items still marked for review. This worksheet does not inspect files or approve a design.
Why a PCB DFM Checklist Matters
Review the hole, layer span and plating requirements together. Original explanatory schematic; not production measurements.
A checklist makes the release review repeatable. It should connect a design feature to a named reviewer, a process response and an approval record. It cannot establish manufacturability simply because every box is ticked.
Start with the current board revision and proposed PCB manufacturing construction. Capture unresolved questions explicitly, including which changes the supplier may propose and who can approve them.
The Complete PCB DFM Checklist: 25 Critical Items
Compare exported data with the intended board. Original explanatory schematic; not production measurements.
1. Minimum drill size
Separate tool diameter from finished-hole diameter and plated from non-plated requirements. Ask whether the proposed hole size and depth fit the selected material and drilling process.
2. Aspect ratio
State the hole depth and diameter basis for each structure. Use the ratio as a geometric descriptor, then obtain process review rather than treating one ratio as an acceptance limit.
3. Drill-to-copper clearance
Review drill registration, plating allowances and required insulation distance together. Check all layers around the hole, not only the visible outer land.
4. Annular ring
Identify the hole type and layer being assessed. Determine land geometry from the applicable requirements and process tolerances; retain the approved drawing and criterion reference.
5. Via-in-pad
Define fill, cap and planarization where required. Review the pad and thermal implications with the BGA assembly process and distinguish proposed options from approved construction.
6. Drill file completeness
Reconcile tool assignments, plated/non-plated definitions and any depth-controlled features with the layer map and drawing. Remove ambiguity about which holes connect which layers.
7. Hole-to-hole separation
Review the remaining material web, drill registration and tool access for adjacent holes. Check mixed plated/non-plated features and routed slots in the same region.
8. Trace width
Specify finished copper width and thickness. Review etching constraints separately from current, temperature-rise and controlled-impedance requirements.
9. Trace spacing
Set spacing from electrical isolation and the fabricator-reviewed process. High-voltage designs may have product safety requirements beyond a generic PCB rule.
10. Copper-to-edge clearance
Use the finished outline and the proposed routing or scoring tolerance. Identify intentional edge contacts or plating so they are not confused with unintended exposed copper.
11. Acute copper geometry
Inspect neck-downs, corners and small copper features in the manufacturing output. Discuss etching concerns in the context of the actual process instead of labeling every acute angle an acid trap.
12. Copper slivers
Check small copper features for intended connectivity and reproducibility. Remove unintended fragments only after confirming that the edit preserves the circuit and required clearances.
13. Thermal reliefs
Review spoke geometry and plane connections against current flow and the soldering process. Check for unintended isolated or partially connected pads after copper pours are regenerated.
14. Plane clearance around holes
Size anti-pads from the hole/land definition, registration allowance and isolation requirements. Check the resulting reference-plane continuity for nearby signals.
15. Plane splits
Verify isolation between voltage regions and check how signals cross or change reference structures. A manufacturing spacing check alone does not establish a sound return path.
16. Copper balance
Discuss copper distribution with the fabricator in the context of the layer stack and lamination process. Any added balancing copper must preserve connectivity, clearance and electrical intent.
17. Thermal-via arrays
Use the component manufacturer’s package guidance and the intended heat path to choose the via arrangement. Review assembly implications where vias intersect solderable pads; a diameter and pitch copied from another device are not a validated thermal design.
18. Mask openings
Review the opening against the pad definition, registration allowance and assembly process. Coordinate mask and paste decisions through the PCB stencil specification.
19. Mask web
Check whether the proposed mask process can retain the intended web between openings. If it cannot, review the pad, mask and assembly alternatives together.
20. Via treatment
Specify open, tented, filled or capped treatment by via class or location. Confirm the selected process and inspection expectations rather than leaving the decision implicit.
21. SMD and NSMD pads
Use the package manufacturer’s land-pattern guidance and assembly review to select the pad definition. Ensure the CAD pad, mask opening and released drawing express the same choice.
22. Legend-to-pad clearance
Check print registration and exclude legend from solderable areas. Inspect the exported legend rather than relying only on the native CAD display.
Match the legend and assembly drawing to the fitted variant. Where a designator cannot be visible on the board, provide an unambiguous location in the assembly documentation.
25. Polarity and orientation
Use consistent pin-one and polarity conventions and verify them against the component documentation. Reconcile placement rotation with the assembly drawing before release.
Review the changed outputs and retain the evidence. Original explanatory schematic; not production measurements.
Review topic
Input and decision
Release evidence
Drills and interconnects
Hole definitions, layer connections, land geometry and via treatment
Reviewed drill/stack drawing and change disposition
Copper and references
Finished geometry, isolation, plane continuity and heat paths
Released copper data consistent with approved constraints
Mask, paste and legend
Pad definition, openings, process clearances and markings
Reviewed fabrication and assembly outputs
Release package
BOM, placement, drawings and acceptance requirements
One revision with open issues closed or explicitly accepted
Use the table as an index to the detailed findings. It does not introduce additional numeric limits or override the approved drawing.
Useful DFM Resources and Tools
Finished hole, layer span and surface treatment are separate. Original explanatory schematic; not production measurements.
Use the CAD rule checker and a manufacturing-data viewer with project-specific constraints. For package details, start with the component manufacturer’s documentation.
An index or application example does not replace the applicable standard or qualify a factory process. Record the exact source, package or construction used in the review.
When to Run DFM Checks
A geometry example is not a manufacturing acceptance limit. Original explanatory schematic; not production measurements.
Before layout: review unusual stack-ups, packages, holes and assembly constraints.
After placement and initial routing: resolve access and construction conflicts while changes are manageable.
Before release: review exported fabrication data and reconcile BOM, placement and drawings.
After an approved change: repeat checks affected by that change and identify the new release revision.
For prototype PCB assembly, define the questions and measurements the build will address. Record what remains unvalidated rather than treating a first article as proof of every operating condition.
Frequently Asked Questions
Inspect final copper connections after the pour is refilled. Original explanatory schematic; not production measurements.
How does DRC differ from DFM?
DRC checks configured CAD rules. DFM reviews whether the actual production package is suitable for the proposed processes. Both need correct inputs and a documented response to findings.
When should the checklist change?
Update affected checks when the design, component package, construction, supplier process or acceptance requirements change. Use build findings to improve specific review steps rather than changing limits without evidence.
Does the supplier review replace the design review?
No. The supplier may identify process issues, while the design owner remains responsible for approving changes against circuit and product requirements. Make the review scope explicit.
What changes for HDI?
Review the actual microvia or other interconnect structure, layer sequence, materials and build process. Confirm the required qualification and inspection evidence; HDI is not a single universal set of trace and via dimensions.
Close and maintain a DFM release record
Opening, stencil and legend decisions need coordination. Original explanatory schematic; not production measurements.
Close the review with a controlled file package and a disposition for every open issue. Keep the approved construction and its assumptions available for repeat orders, and re-review changes that affect them. A useful DFM checklist produces decisions and traceable records, not unsupported guarantees.
Review the hole, layer span and plating requirements together. Original explanatory schematic; not production measurements.
A useful PCB DFM checklist connects each manufacturing question to an identifiable feature, an agreed requirement and a release decision. Passing a CAD rule check is one part of that process. It does not prove that the exported files describe the intended revision or that the chosen construction is compatible with a particular fabrication process.
The following 25 checks are organized into six review stages. Use them to prepare a fabrication package and resolve questions before committing to production. Numerical limits must come from the agreed construction and process capability, not from a generic table copied into every project. The worked geometry example is illustrative and does not state a PCBSync manufacturing tolerance.
1. Establish the release package before reviewing geometry
Compare exported data with the intended board. Original explanatory schematic; not production measurements.
Check 1: revision identity. Give the PCB, fabrication drawing and exported data a consistent identifier. State the layer count and board revision, and distinguish the bare-board release from an assembly variant. If a filename includes a revision but its contents were exported earlier, the filename alone provides no protection.
Check 2: output inventory. List the required copper, mask, legend, outline and drilling or routing information. Identify the format and units. The receiving fabricator needs to know which files are authoritative and which are explanatory views. Remove superseded alternatives from the release folder rather than expecting someone else to select the newest-looking file.
Check 3: independent output review. Open the exported manufacturing data in a viewer and compare it with the intended board. Look for missing layers, incorrect polarity, offsets and absent holes. The Gerber format documentation explains how layer images and associated attributes carry fabrication information; a successful export is not itself a review of the exported result.
Check 4: agreed requirements. State material, thickness, copper, surface finish, acceptance requirements and any special construction instructions. Link each unusual requirement to a drawing feature or note. If a requested value differs between the order form and fabrication drawing, resolve that conflict instead of allowing the factory to guess which document takes precedence.
For each check, retain a short evidence record: the file or feature reviewed, the requirement, the finding and the owner. This keeps the review usable after an engineering change. A checklist containing only ticks cannot show whether the reviewer examined this revision or a previous export.
2. Review holes, via structures and routing as a coordinated set
Finished hole, layer span and surface treatment are separate. Original explanatory schematic; not production measurements.
Check 5: hole definition. Distinguish a finished plated-hole requirement from a nominal tool size. Identify non-plated holes and slots explicitly. Review tolerances against their function, such as a press-fit interface or mechanical alignment, rather than assigning the same tolerance to every hole.
Check 6: layer span and plating. State which layers each blind, buried or microvia structure connects. Check that the drill or fabrication information expresses that construction unambiguously. A drawing that only says “blind vias” leaves important manufacturing questions unanswered.
Check 7: annular ring and drill-to-copper clearance. Review pad, hole and clearance geometry together with the applicable registration and processing allowances. Keep design dimensions separate from acceptance criteria on a finished board. Ask how the fabricator interprets the relevant dimensions before trying to approve them with a simple subtraction.
Check 8: aspect ratio and sequence. Assess the actual via depth and hole geometry for the proposed process. Through-hole and microvia constructions should not share an unexplained generic ratio limit. Lamination sequence, filling, plating and qualification evidence can matter as much as a single ratio.
Check 9: fill, cap and surface condition. For via-in-pad or other treated vias, describe the required result and applicable process, including whether a solderable surface is needed. “Tented,” “filled” and “capped” are not interchangeable instructions. Confirm the definition with the supplier.
Check 10: mechanical features. Check hole-to-hole, hole-to-edge, slot and cutout relationships against the proposed routing and drilling process. Include any edge plating, castellations or controlled-depth features in the review. The release output is an agreed construction, not merely a list of drill diameters.
3. Check copper geometry against electrical purpose and fabrication constraints
Inspect final copper connections after the pour is refilled. Original explanatory schematic; not production measurements.
Check 11: minimum conductor features. Identify the narrowest traces, neck-downs and isolated copper features on each layer. Review the selected copper construction and process rather than assuming one width applies equally to every layer. A short escape feature may need its own discussion; it should not be hidden by a larger nominal track width.
Check 12: spacing and isolation. Review the smallest gaps, plane separations and clearance regions. Electrical safety requirements and manufacturing spacing are different questions. A feature that can be etched is not automatically acceptable for the product’s voltage, environment or applicable safety requirements.
Check 13: connections after final copper refill. Inspect thermal reliefs, narrow spokes, isolated islands and connections around clearance regions. Re-run the relevant checks after modifying pours. The KiCad PCB Editor documentation describes configurable design-rule checking; its output still depends on the constraints and data supplied to the tool.
Check 14: copper near the finished outline. Review traces, planes and exposed copper relative to the actual routed or scored boundary. State where exposure is intentional. Avoid treating a drawing line, a tool centerline and a finished board edge as the same reference.
Check 15: stack-up and impedance coordination. Make sure the proposed material and dielectric construction can support the required impedance geometry. Record which dimensions may be adjusted and which need design approval. Uncontrolled changes to a trace width or reference layer can resolve a fabrication issue while changing electrical behavior.
Check 16: copper distribution. Discuss imbalance and any proposed nonfunctional copper with the fabricator. Do not automatically add copper into RF, isolation or antenna regions just to reach a percentage target. Document the electrical restrictions and agree where process-related additions are permitted.
4. Keep solder mask, paste and legend requirements distinct
Opening, stencil and legend decisions need coordination. Original explanatory schematic; not production measurements.
Check 17: mask opening intent. Confirm whether a particular pad is mask-defined or copper-defined and verify that the package and assembly guidance support that choice. Treat an opening dimension as a design decision with process implications, not as a universal expansion value.
Check 18: remaining mask webs. Review the smallest web between adjacent openings against the selected mask process and registration allowance. If the intended web cannot be retained, agree the alternative and assess the assembly implications before releasing the data.
Check 19: vias and mask treatment. State which vias are open, covered or otherwise treated. Mask coverage is not the same as a filled via. Do not assume that a covering instruction establishes a flat, solderable surface beneath a component.
Check 20: paste data ownership. Keep the stencil requirements and paste apertures aligned with the assembly process. A bare-board mask change should not silently modify the intended paste strategy. For assemblies supplied with customer stencil data, identify who reviews aperture changes and how approval is recorded.
Check 21: legend clearance. Keep ink away from solderable areas and from features where markings could interfere with inspection or assembly. Inspect the exported legend after clipping or other processing. Automatic clipping can protect a pad while removing an important polarity mark.
Check 22: legibility and identification. Confirm that essential reference designators, polarity marks and revision identifiers remain readable and unambiguous. A component outline can help orientation, but it is not a substitute for a clear assembly drawing. Preserve the distinction between a manufacturing aid and a requirement that must appear on the finished board.
5. Work through tolerance questions instead of quoting a minimum
A geometry example is not a manufacturing acceptance limit. Original explanatory schematic; not production measurements.
Consider an illustrative circular pad with diameter 0.60 mm and a nominal hole diameter of 0.30 mm. If the two circles are concentric, their geometric radial difference is (0.60 − 0.30) / 2 = 0.15 mm. This is a starting geometry calculation, not a statement of finished-board acceptance.
Now assume, solely for the example, that the hole center is displaced by 0.05 mm relative to the pad center. In the direction of displacement, the idealized remaining radial width is 0.15 − 0.05 = 0.10 mm. This model ignores size variation, layer registration, pad processing and other allowances. It therefore cannot be promoted into a universal annular-ring rule.
The useful engineering question is which dimensions and tolerances govern the actual requirement. Ask whether the hole dimension refers to the finished hole or a tool, which layer is being assessed, how registration is specified, and what acceptance definition applies. Put the answers in the fabrication record rather than presenting the arithmetic as proof of reliability.
Check 23: panel and separation requirements. Review rails, tooling, support, tab locations, scoring or routing and component proximity where assembly is relevant. State whether the customer or supplier owns the panel design and which changes require approval. A finished-board drawing does not fully describe the manufacturing panel.
Check 24: inspection and electrical test scope. Agree what evidence is required and how it relates to the released design. Distinguish a bare-board electrical test from assembled-product functional testing. Clarify any required coupons, dimensional records or other verification before they become a late order change.
This stage turns vague questions into bounded decisions. A supplier response should identify the feature and proposed action, so that the designer can assess electrical, mechanical and assembly consequences together.
6. Close the review with an auditable release decision
Review the changed outputs and retain the evidence. Original explanatory schematic; not production measurements.
Check 25: exception closure. Every finding needs a disposition tied to the current revision. For a correction, identify the changed file and the repeated check. For an accepted exception, record the owner, scope and conditions. Keep unresolved findings open rather than converting them into approval through a general email saying that the order may proceed.
Separate commitments where appropriate. Purchasing a material, manufacturing a stencil and starting fabrication may not require the same approval. State which work is authorized and which remains on hold. This avoids an apparently minor unresolved detail becoming expensive because another operation has already started.
After an engineering change, revisit the affected checks and their dependencies. Moving a connector can affect the outline, drill information, mask, legend, assembly access and panel separation. Re-export the complete affected data set and compare it with the approved release package. Do not mix corrected files into an old folder without a clear manifest.
Keep a final package containing the reviewed data, drawing, agreed construction, exception register and approval record. Record the supplier’s questions and the corresponding designer responses. This record makes repeat orders and later investigations more straightforward, even when the people involved in the original release are no longer available.
For a PCB manufacturing quotation, provide the current fabrication data and drawing, material and stack-up requirements, quantity, delivery expectations and any unresolved features. Include the BOM and assembly files if assembly is part of the project. Discuss the DFM review scope with PCBSync before treating a general checklist as approval for a specific construction.
KEEP EXPLORING
Related engineering articles
Continue with practical guides connected to this topic.